Strong Magnet Manufacturer Tips for Sourcing Durable Neodymium Magnets
2026-09-17
Finding a supplier who truly understands durability in neodymium magnets is harder than it sounds. Many claim strength, but few deliver consistency over time. If you're sourcing magnets that need to perform under real-world stress—temperature shifts, corrosion, or repeated impact—you've likely run into the gap between spec sheets and reality. At DAWA, we've seen what goes wrong when buyers overlook key manufacturing details, and we're sharing those lessons here. This guide breaks down the practical tips you won't find in a generic catalog, helping you avoid costly mistakes and choose magnets that actually last.
Pin Down the Exact Grade Before You Sample
Too many sampling campaigns stumble because the grade was never confirmed before the first bag was filled. A hand-drawn map or an old rumor about high values is not the same as pinning down the exact grade. When you skip that step, everything downstream—from the spacing of your sample stations to the number of duplicates you send to the lab—gets built on a shaky assumption. Field crews often end up re-walking the same ground after the lab returns numbers that make no sense against what they saw in the pit.
Confirming the grade ahead of time does not require a full drill program. A few well-placed chip samples, a quick handheld XRF scan, or even a careful review of nearby assay certificates can usually settle the question. Once you have that number in front of you, the sampling protocol stops being a guess. You can shorten intervals where the grade swings hard, widen them where it holds steady, and skip sending obviously barren material to an expensive laboratory. That is the difference between a tight, defensible dataset and a pile of numbers nobody trusts.
Skipping the upfront confirmation often looks like saving a day of fieldwork, but it almost always costs more later. You end up resampling, relogging, or rewriting the report because the original numbers never matched the ground truth. Pin down the exact grade first, and every sample after that has a solid reference point to lean on.
Insist on Salt Spray Testing for Coated Magnets
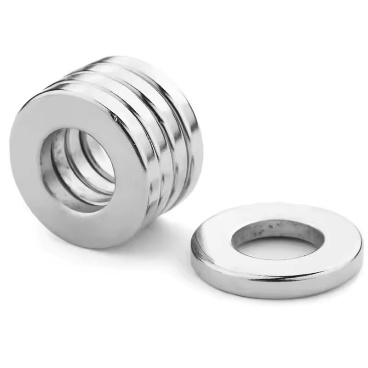
Salt spray testing is not an optional extra for coated magnets; it exposes pinholes and weak spots that visual inspection will never catch. A nickel-copper-nickel or epoxy coating can look flawless yet fail within hours under continuous salt fog. Always ask for raw ASTM B117 test reports with exact exposure hours and sample photos, not a summary that simply says the coating passed.
The failure modes are predictable but still easy to miss without testing. Blisters, rust spots, and edge lifting are common after salt exposure. A single pinhole lets moisture reach the neodymium substrate, starting oxidation that swells and cracks the coating from underneath. Insisting on salt spray testing before accepting a shipment costs far less than replacing magnets that corrode after installation.
Match the test duration to the actual use environment. A magnet that survives 24 hours in a salt spray chamber might be fine for indoor use but worthless in marine or coastal conditions. Require 48, 72, or even 200+ hours depending on exposure, and demand photos of the samples after testing. If the supplier pushes back on sharing raw salt spray data, treat that hesitation as a warning sign.
Ask How They Handle Hydrogen Embrittlement
Hydrogen embrittlement doesn't announce itself with a crack or a hiss—it waits until the part is under load, often weeks after plating or pickling. A shop that truly understands this failure mode won't just nod when you mention it. They'll walk you through their baking procedures, the controls on acid exposure, and how they validate that trapped hydrogen has actually been driven out. Ask them what happens if a batch gets delayed between cleaning and baking. If the answer is a shrug, keep looking.
The best fabricators treat hydrogen relief as a process variable, not a checkbox. They'll tell you the specific temperature and soak time they use for high-strength steels, and they'll show you records proving it happened—not just a log that says "baked." Push them on how they handle parts with hardness above 40 HRC, where the risk shoots up. A good shop will mention reduced acid immersion, mechanical cleaning alternatives, or immediate baking windows. If they've never had a hydrogen-related failure, that's either luck or a sign they don't inspect closely enough.
Also listen for the language they use. Do they blame the plating vendor when a bolt snaps? Do they suggest baking everything "just in case" without knowing the material spec? That's the opposite of expertise. A capable fabricator will ask about your alloy, your service environment, and whether you've seen delayed fractures before. They'll recommend a preventive path—maybe a different coating, maybe a design change—not just a generic heat cycle. That conversation tells you more about their metallurgical depth than any certificate on the wall.
Map Out the Full Magnetic Field, Not Just Surface Gauss
Surface gauss readings are easy to grab, but they only show a tiny slice of what the magnet is actually doing. A single point on the face might read 3,000 gauss while just a few millimeters away the field drops or bends sharply. If you design around that one number, you overlook hotspots near edges, dead zones in the center, and the way flux spills out from the sides.
The real behavior lives in the spatial map—how the field vector changes across every axis, not just perpendicular to the surface. For a sensor placed at an angle or a reed switch sitting off to one side, that directional information matters more than peak face gauss. You can see this when you sweep a probe across a magnet array: the strongest pull is rarely where the sticker says it should be.
A practical way to build that full picture is to combine coarse grid measurements with simulation, then verify a few critical points on the bench. Plotting field lines, not just colored dots, reveals where flux loops back and where it cancels. Once you have that map, your mounting tolerances, shielding choices, and even magnetization direction stop being guesswork.
Clarify Lead Times for Custom Shapes and Tolerances
Custom geometries and tight tolerance callouts rarely share a single lead time. The moment a drawing includes a non-standard profile or a tolerance stack that pushes past standard manufacturing limits, the schedule shifts. We ask for specifics early: which features drive the longest operations, whether special tooling or fixturing is needed, and whether inspection will require CMM time beyond routine checks.
Rather than quoting a generic 4–6 weeks, we break the timeline into segments—material sourcing, programming, setup, first-article verification, and any secondary finishing. This makes it easier to see where a custom shape adds days versus where a tolerance refinement simply adds inspection hours. If a feature can be relaxed without affecting function, that change often brings the date back in.
For true custom work, we also distinguish between first-article lead time and repeat order lead time. The first run includes prove-out and possibly iterative adjustments; later runs should be faster once the process is stabilized. Confirming these expectations up front avoids surprises and keeps everyone working from the same schedule.
Get a Clear Picture of Scrap Recovery and Pricing
Understanding scrap recovery starts with knowing exactly what materials you're dealing with. Different alloys, coatings, and contamination levels shift the value significantly, so a quick visual check or a simple magnet test isn't enough. Real clarity comes from consistent sampling and working with buyers who explain their grading criteria rather than hiding behind vague categories.
Pricing often feels like a moving target because spot markets for copper, aluminum, and steel can swing within a single week. Instead of chasing daily quotes, build a baseline by tracking your own recovery volumes and comparing offers from at least three reputable yards. That way you can spot when a lowball number reflects market conditions versus when someone is simply trying to take advantage of you.
The most overlooked part of getting a clear picture is recording the condition of scrap before it leaves your site. Photograph loads, note moisture or dirt content, and keep a simple log of accepted weights versus your own estimates. Over time, these records become your negotiation tool, helping you push back on deductions and secure pricing that actually matches the quality you deliver.
FAQ
A standard nickel-copper-nickel triple layer works for basic indoor use, but if moisture or salt spray is involved, ask for epoxy, PTFE, or parylene coatings. Inspect the coating for pinholes and even coverage, and request a neutral salt spray test report showing hours to first red rust.
Look at the letter suffix after the grade, such as N35SH, N42UH, or N48EH. These letters indicate the maximum working temperature before irreversible losses begin. A trustworthy manufacturer will also share a demagnetization curve or high-temperature test data, not just a catalog value.
Not always. Very high grades like N52 are more brittle and often cost more per unit of magnetic output. If an N35 or N42 magnet already meets your force requirement and the working temperature is within its range, the extra money rarely buys meaningful durability. Focus on the actual operating point in your magnetic circuit instead of chasing the highest number.
Sintered neodymium blanks have loose tolerances, but a capable factory with grinding and machining can typically hold plus or minus 0.05 mm on most dimensions, and tighter for thin or small parts. Send a clear drawing with critical dimensions flagged, and ask whether they do in-house precision grinding or only resell rough blanks.
Ask for a batch-specific test report covering magnetic flux, surface field, or a full BH curve. Independent third-party testing is even better. For your own incoming inspection, use a calibrated gauss meter and a pull-force tester, but keep your method consistent, because measurements taken at different points or gaps will not be comparable.
Yes. The source and quality of rare earth material directly affect coercivity and batch consistency. If a supplier cannot or will not say whether they use virgin alloy, recycled material, or mixed feedstock, that is a warning sign. Request material composition certificates or grade traceability, and be suspicious of prices that seem far below the market.
Custom shapes are possible, but sharp corners, thin walls, or deep slots increase the risk of cracking during sintering, machining, or magnetizing. Design with generous radii and avoid sudden cross-section changes. Ask the manufacturer to review your geometry for manufacturability and provide prototype samples for real-life testing before committing to a production run.
Order small sample batches and test them under your actual conditions, including temperature cycling, humidity exposure, and mechanical shock. Check whether the supplier holds ISO 9001 or IATF 16949 certification and whether they operate their own sintering and coating lines rather than acting as a trading company. Responsiveness, engineering support, and willingness to discuss failure modes often reveal more than a quote sheet.
Conclusion
When sourcing neodymium magnets from a strong magnet manufacturer, you need to move past generic datasheets and push for specifics that affect real-world durability. Pin down the exact grade—like N42, N48SH, or higher—before you request samples, because grade choice dictates temperature stability and coercivity, and a sample built on the wrong grade can mislead your entire design validation. Once the grade is settled, insist on salt spray testing for any coated magnet; a shiny nickel-copper-nickel layer can hide poor adhesion or pinholes that rust within weeks in humid environments. At the same time, ask directly how the manufacturer handles hydrogen embrittlement, a silent killer for high-strength magnets used in plated assemblies. A reputable shop will have a baking or pre-plating process to drive out hydrogen, not just shrug off the question.
Beyond material integrity, map out the full magnetic field rather than relying on a single surface gauss reading. Ask for flux density curves or simulation data across your operating gap, especially if the magnet works in a dynamic or off-axis setup. Custom shapes and tight tolerances come with lead times that vary wildly between suppliers; clarify upfront whether they handle in-house wire EDM, grinding, or only standard blocks and discs. Finally, get a clear picture of scrap recovery and pricing. A transparent manufacturer should explain how they credit returned magnet scrap or machining waste, which can offset costs on large production runs and signals honest material accounting. These checks separate a durable magnet partner from a vendor that simply sells you a shiny metal piece.
Contact Us
Contact Person: Kelvin Lo
Email: [email protected]
Tel/WhatsApp: 0769-88561131
Website: https://dawamagnetic.com/